Product infeed
Review pack width, length, height, stability and spacing before selecting the infeed and sealing frame configuration.
Automatic L-sealers and shrink tunnels specified for your pack size, film and output.
Compare L-sealer application tests Use the actual pack construction and cooled finish to decide whether the wrapping route is suitable.
Built for shrink wrapping projects
L Sealer Machines UK is a focused Lancing UK microsite for buyers comparing semi-automatic, automatic and integrated L-sealer routes. It explains how an L-sealer fits with a heat tunnel, what information is needed for a quotation, and how to shortlist machinery around real product dimensions rather than a generic brochure description.
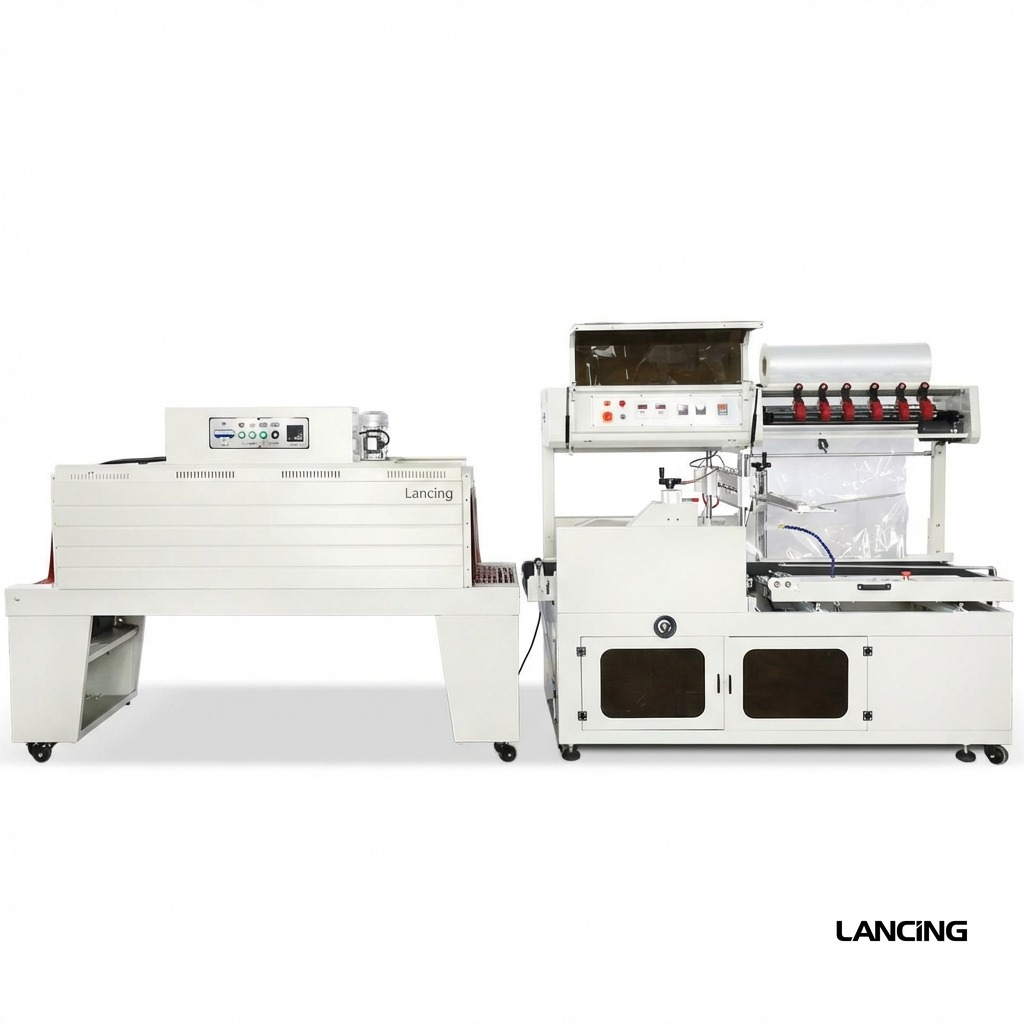
The featured LU-SPL6 route combines automatic sealing with a shrink tunnel for POF and PE film applications. It is aimed at production teams that need cleaner pack presentation, more stable throughput and practical support with line layout.
L-sealer selection guidance
Buyers often search for an L sealer machine, shrink wrapping machine, heat tunnel, chamber sealer or automatic shrink wrapping line before they know which route is correct. The correct recommendation depends on the product dimensions, film type, pack stability, required packs per minute and the quality of finish expected after the heat tunnel.
Lancing UK can help compare automatic L sealers, semi automatic L sealers, chamber sealing machines, sleeve sealers and shrink tunnel machinery so the quotation matches the production requirement instead of a generic catalogue listing.
Machine route
The route is specified around the product, film, seal quality and heat-shrink finish required from your line.
Review pack width, length, height, stability and spacing before selecting the infeed and sealing frame configuration.
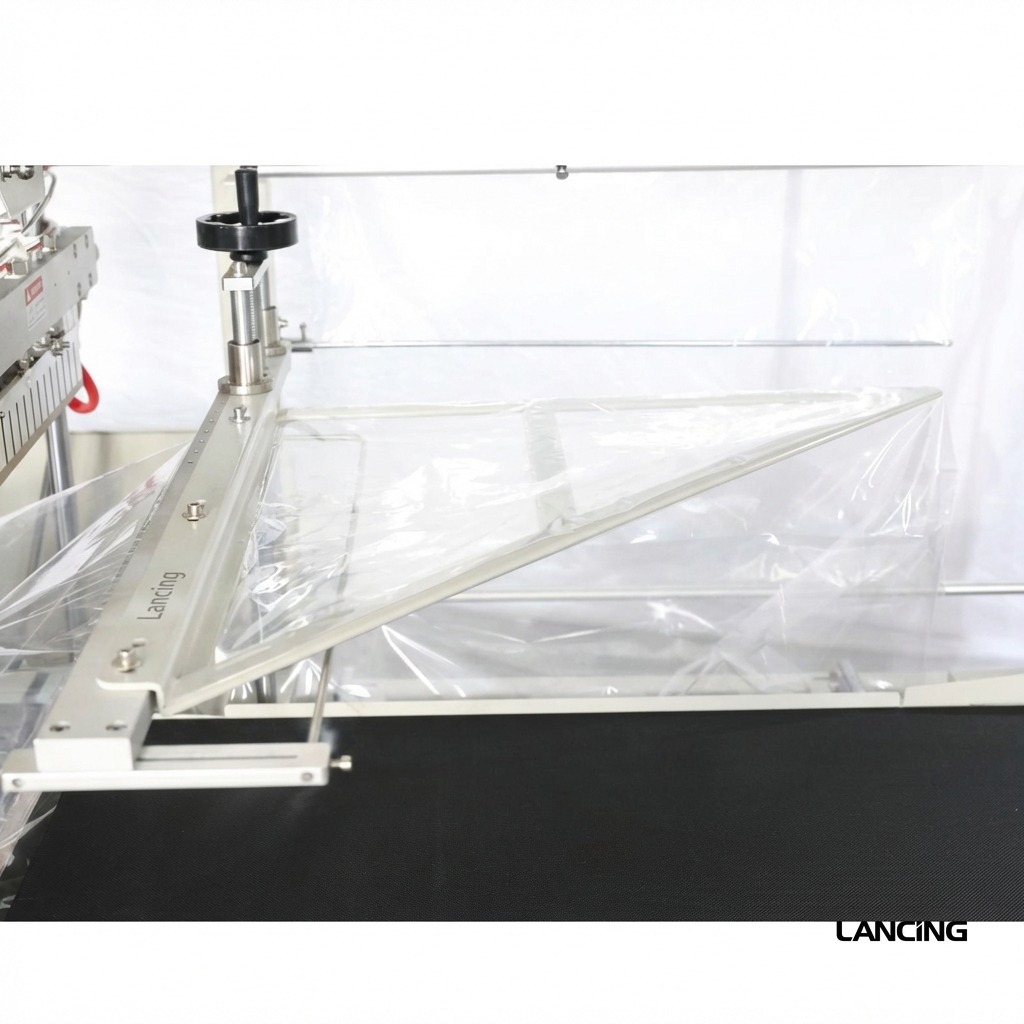
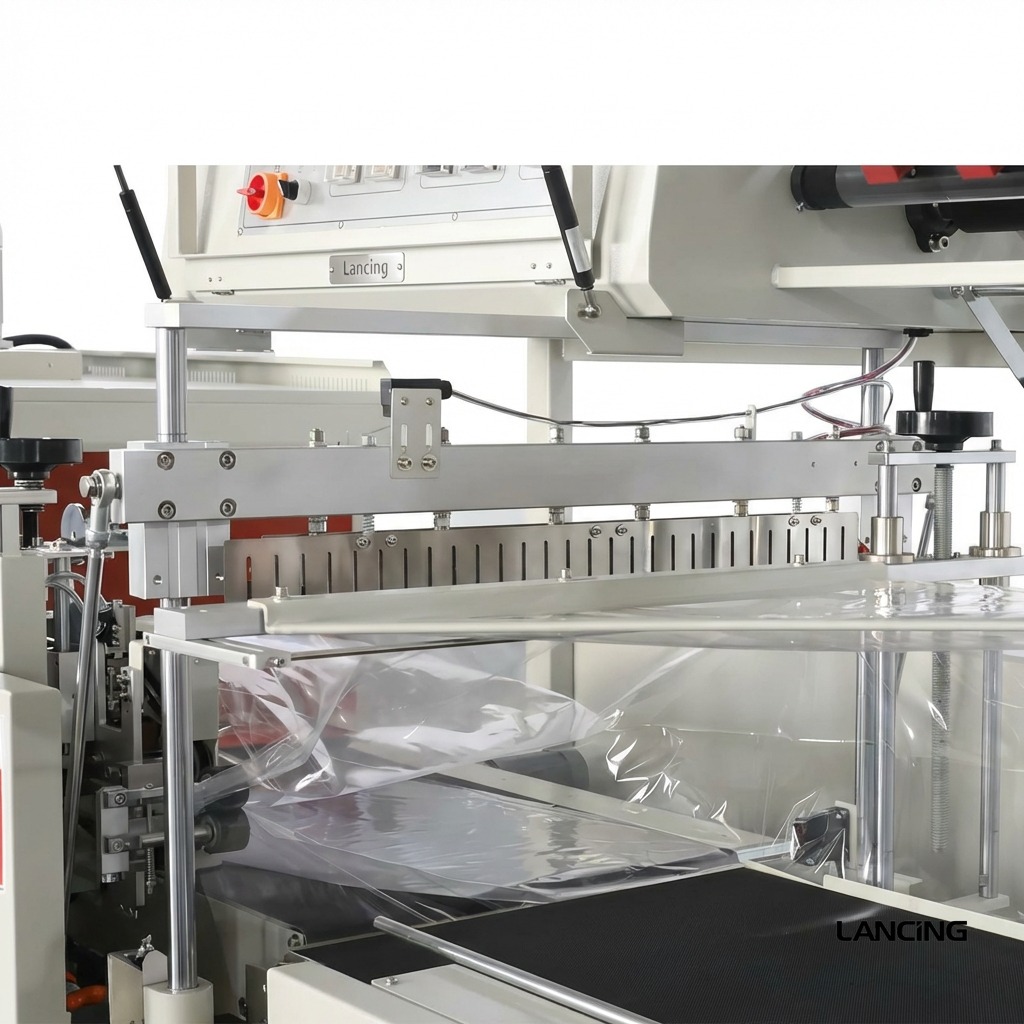
The seal stage creates the loose shrink-film bag around the product, with the seal quality dependent on film type, temperature and product handling.
The tunnel applies controlled heat to tighten the film and create the finished pack presentation before outfeed or end-of-line packing.
Product range
Build the line around the pack. Alongside automatic L-sealers, the range can include chamber sealers, sleeve sealers, heat tunnels, sleeve applicators and flow wrappers.

Compact chamber shrink wrapping for small boxes, kits and retail items.
View product range →
Automatic film folding, L-sealing and cutting for repeat production.
View product range →
Shrink sleeve sealing for trays, multipacks, bottles and grouped cartons.
View product range →
Controlled heat-shrink tunnels matched to film, pack dimensions and speed.
View product range →
Applicators for shrink sleeve labelling and tamper-evident sleeve work.
View product range →
Horizontal wrapping routes for individual packs, bars, bakery and similar products.
View product range →Featured model
This configuration supports automatic shrink wrapping with side sealing and heat shrinking in one line. It is suited to boxes, books, cartons, electronics, retail packs and similar products where the seal and shrink finish need to be controlled.
Applications
L-sealers are typically considered where a product or grouped pack needs a tidy, enclosed shrink wrap rather than only a transit sleeve. They can support food, print, cosmetics, household goods, industrial products and contract packing projects.
Quick answers
An L sealer machine wraps a product in shrink film and seals the film on two sides in an L-shaped seal before the pack moves to the shrink stage.
L-sealers are commonly used for cartons, trays, boxes, printed packs, retail packs and grouped products where a neat shrink finish is required.
Yes. The team can review pack dimensions, film type, output target, utilities and line layout before recommending a suitable L-sealer, heat tunnel or wider shrink wrapping system.
Common buying questions
These pages answer the main buying questions that usually come before an L-sealer quotation.
For carton and retail pack lines that need a complete sealing and shrink tunnel route.
Understand the specification details that change machine cost and layout.
Compare L sealers, chamber sealers, sleeve sealers and heat tunnels.
Engineering selection guidance
A strong L-sealer specification starts with the pack, not the machine catalogue. The product height, film centre-fold width, seal position, tunnel opening, airflow and cooling space all affect whether the final pack looks tight and repeatable. For that reason, Lancing reviews the product dimensions, film type and target throughput together before recommending an automatic L sealer, semi automatic L sealer, chamber sealer or sleeve sealer route.
The LU-SPL6 information already shown on this site includes a listed 15–30 bag/min operating range and POF / PE film compatibility. That figure should be treated as application-dependent: product size, film thickness, operator feed consistency, tunnel temperature, dwell time and discharge cooling can all change the practical output on a real line.
This site stays focused on L-sealing and shrink tunnel applications. Where a sleeve sealer, flow wrapper or general shrink wrapping route is more appropriate, the specification should be separated so the L-sealer page does not compete with those specialist routes.
| Selection point | What to confirm | Why it matters |
|---|---|---|
| Pack size and stability | Confirm the largest product width, length and height, plus whether the product can move inside the film before shrinking. | The sealing frame, infeed spacing and tunnel aperture must all suit the actual pack, not only the smallest sample. |
| Film centre-fold and material | Confirm POF or PE film, centre-fold width, thickness and perforation needs. | Film choice affects seal dwell, tunnel behaviour, cooling and the finished pack appearance. |
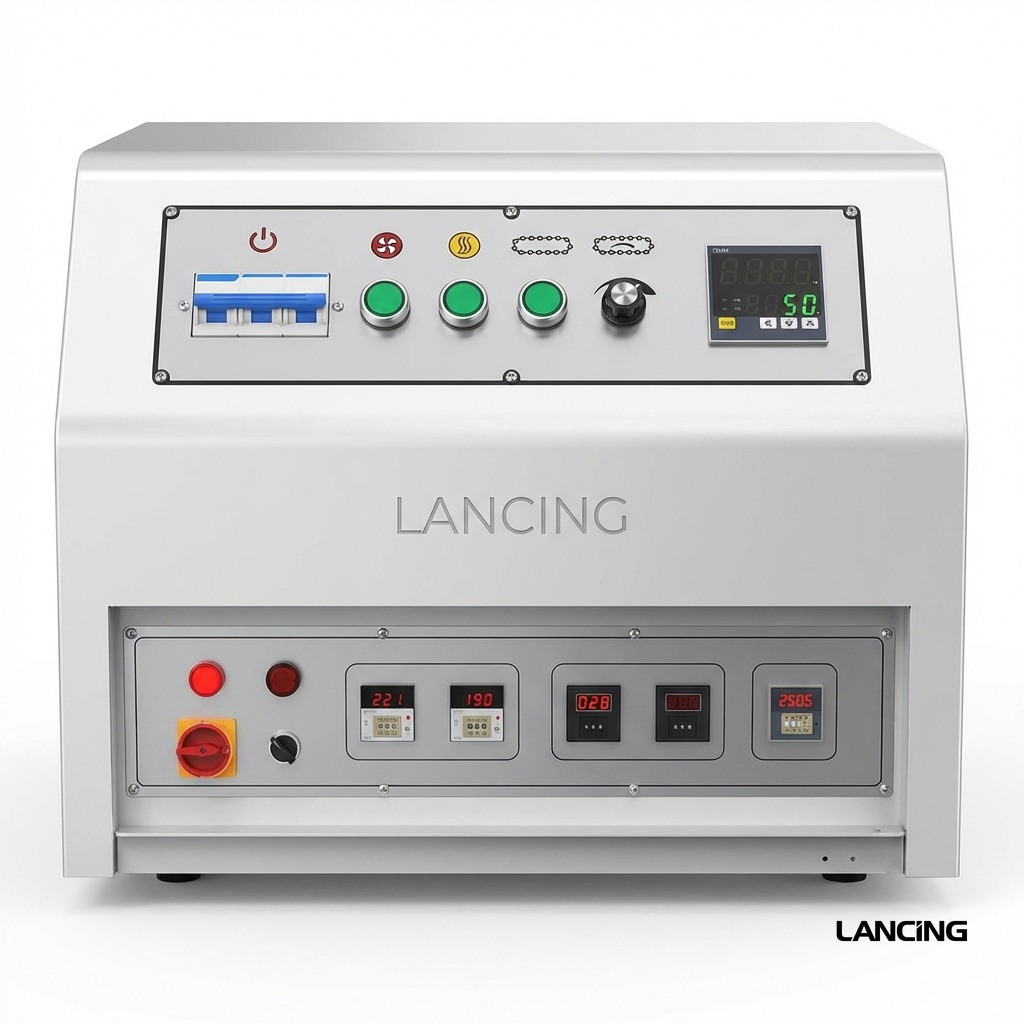
| Heat tunnel settings | Review temperature, conveyor speed, airflow and cooling space during a sample trial. | The tunnel finish is often what decides whether a technically sealed pack is commercially acceptable. |
| Line integration | Check infeed, outfeed, conveyor height, accumulation and operator access. | A suitable sealer can still underperform if the product feed or discharge route is not controlled. |
Compare POF and PE film by product size, presentation requirement and seal behaviour before ordering a machine.
Review temperature, airflow and dwell time together rather than treating the shrink tunnel as a separate afterthought.
Use sample packs and film to prove seal location, tunnel finish and output assumptions before final specification.
No. The listed LU-SPL6 speed is application-dependent and should be confirmed against product size, film, operator feed, tunnel settings and required pack finish.
Automatic L sealers are usually considered when repeat production, conveyor feed and a separate heat tunnel are needed. Chamber sealers can suit lower-volume batch work and compact products.
The useful details are film type, thickness, centre-fold width, roll dimensions, perforation requirement and the pack finish expected after shrinking.
Yes. The route should be matched to the product and presentation requirement; sleeve sealing and flow wrapping can be more suitable for some grouped packs or horizontal wrapped products.
Photos, dimensions, sample products, target output, film details, layout constraints and a short description of current packing problems all make the recommendation more accurate.
Related guidance: Automatic L sealer machines · LU-SPL6 detail · Buyer guide · Enquiry checklist
Agree factory and site acceptance checks and finished-pack criteria before the sample run. Include infeed spacing and product detection in the line review.
For printed film, review registration. The sample-pack video guide and project specification template organise the remaining evidence.
Accurate product dimensions, film type, target output, pack photos, site layout and a clear finished-pack standard usually improve the quality of the recommendation.
A shrink-wrapped finish requires a heat-shrink stage, but the correct tunnel depends on product size, film and the expected finish.
Yes. Sample products, photos or video can help confirm whether L-sealing, chamber sealing, sleeve sealing or another route is more suitable.
Buyer answers
The most useful early answers separate what can be screened from dimensions from what must be proved with real film and sample packs. These questions help buyers describe the application without treating a catalogue limit or headline speed as a finished specification.
Direct answer: Pack dimensions can support an initial feasibility check, but they cannot prove the seal quality, shrink finish or practical output.
Length, width, height and orientation help screen the sealing opening, film width, tunnel aperture and conveyor route. Final suitability can still depend on weight distribution, surface finish, sharp edges, trapped air, heat sensitivity and how consistently the product arrives at the machine.
Direct answer: Products with the same measured envelope can need different film, seal, tunnel and conveyor settings because their materials and behaviour are different.
A rigid printed carton, a flexible bundle and a light gift set can share the same outer dimensions yet respond differently to film tension, hot air, conveyor contact and cooling. The product surface, thermal mass, centre of gravity and ability to release trapped air all affect the result.
Direct answer: Finished appearance is created by the complete film, sealing, shrinking and cooling sequence rather than by one setting in isolation.
Film grade and width determine the material available around the pack; the seal position sets the starting geometry; tunnel airflow, dwell time and temperature recover the film; and cooling stabilises the result. Changing only the tunnel temperature can hide the real cause of wrinkles or loose corners.
Direct answer: A sample run is more useful whenever pack quality, heat exposure, product stability or mixed-SKU handling matters as much as cycle rate.
A speed figure is meaningful only for the product, film, spacing, operator method and tunnel conditions under which it was achieved. Representative samples show whether the line can detect, seal, transfer, shrink and cool the real pack while meeting the buyer's acceptance standard.
Related guidance: How an L sealer works · Quotation comparison checklist · Sample testing guide
Quotation readiness
Direct answer: The most useful L-sealer enquiry evidence is a combination of product dimensions, film details, target output, finished-pack expectations, site layout and sample-pack behaviour. This lets Lancing compare automatic L sealers, semi-automatic L sealers, chamber sealers, sleeve sealing and tunnel options against the real production task rather than a generic machine category.
| Buyer question | Evidence to send | Best supporting page |
|---|---|---|
| Will the machine physically suit the pack? | Largest product dimensions, pack stability, photos and intended orientation. | What size L sealer do I need? |
| Will the film seal and shrink correctly? | Film type, centre-fold width, thickness, perforation and required finish. | Film and seal-window testing |
| Will it fit the production area? | Floor space, working height, utilities, infeed, outfeed and cooling space. | Site preparation and utilities |
| Can it run reliably in line? | Product feed, detection point, upstream/downstream signals and fault recovery. | Controls and sensor integration |
The starting decision is how the film should enclose the product and what the finished pack must look like. Compare the sealing concept and shrink stage with the same representative products.
An automatic L-sealer is a route to assess where the product needs an enclosed shrink-film pack and repeat conveyor handling. Check the largest envelope, unstable products and the required display face before reviewing the sealing frame and film width.
Use the sleeve-sealer range when comparing a sleeve-style bundle. Confirm how the group is formed and supported, whether open ends are acceptable and what strength or presentation the finished bundle needs. A similar output figure does not make sleeve sealing and L-sealing interchangeable.
Compare chamber sealing and semi-automatic L-sealers where manual loading is part of the planned workflow. Include product preparation, handling, cooling and changeovers when judging the useful batch output.
Inspect the unshrunk seal, the pack leaving the tunnel and the cooled result. Record distortion, open seams, trapped air and unwanted contact marks. The film and seal-window guide helps separate the stages before changing settings.
Provide arrival spacing, conveyor heights, available floor space, utilities and downstream handling. Agree what happens when the tunnel or discharge is unavailable. Use the shrink-wrap line-integration guide to connect accepted pack quality with sustained line operation.
An L-sealer project should begin with the presentation standard expected after shrinking and cooling. Keep an unwrapped product and an accepted wrapped example together. Mark the important faces, visible seals, barcode position and any areas where film gathering would be unacceptable. This turns a general request for a neat wrap into something that can be assessed.
Record the full range of product geometry, including changes in height and shape. Two cartons with similar length and width may need different film and handling arrangements if one is taller, lighter or less stable. Include the intended orientation through the machine and the way products arrive at the infeed.
The sealing and tunnel stages should then be reviewed as a connected process. Agree which film will be used, how the loose enclosure is inspected and how the final cooled pack is judged. Keep a record of changes made during a trial so the accepted result remains linked to the actual product, material and operating conditions.
The seal is one part of the result. Assess the film enclosure, tunnel finish, cooled product condition and intended downstream handling against the agreed pack standard.